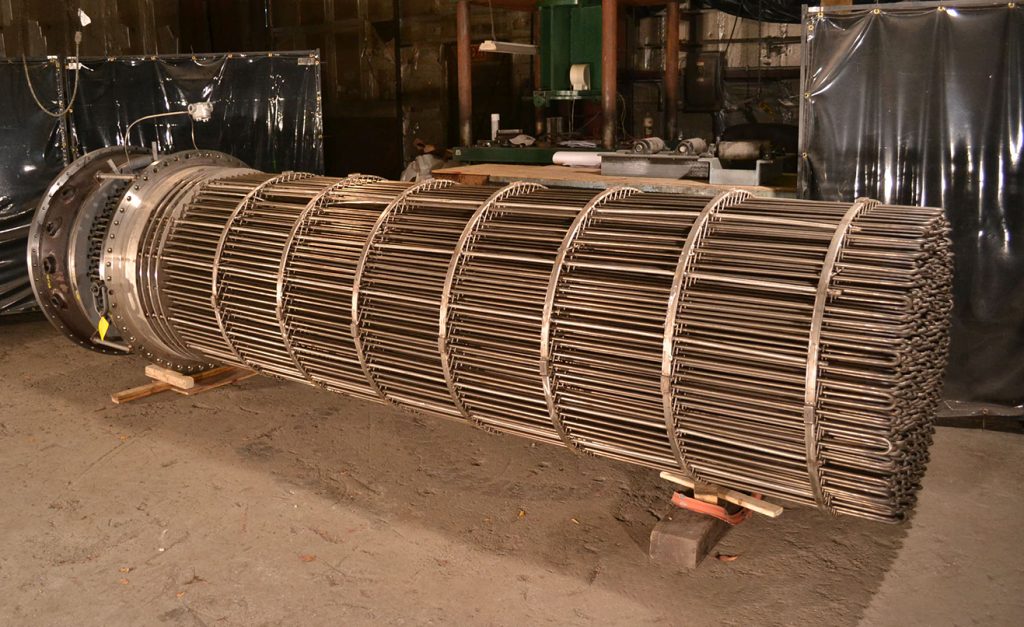
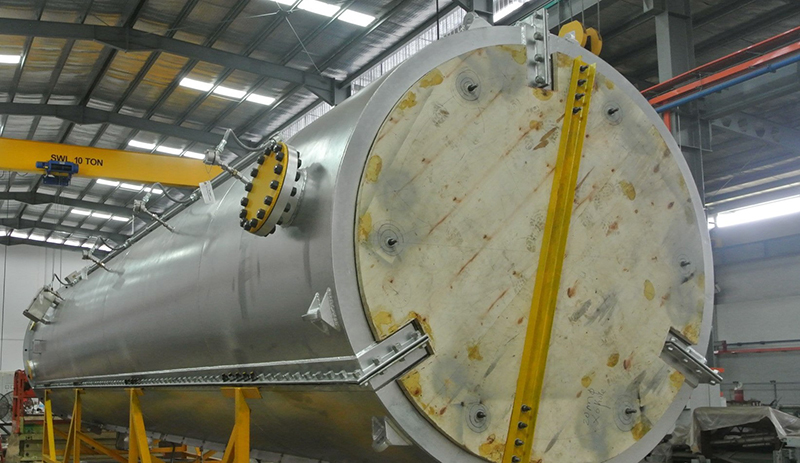
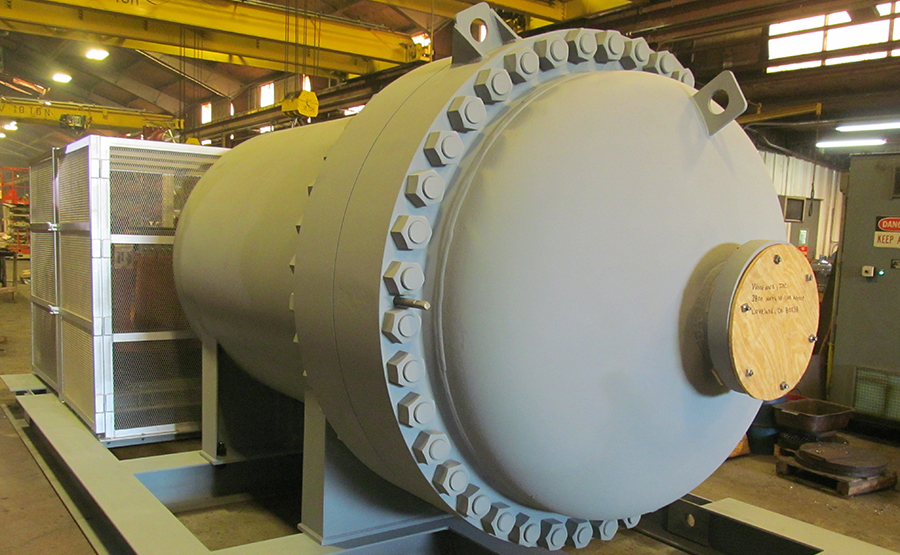
An electric immersion heater shares many visual similarities with a shell and tube type heat exchanger and appears to be a u-tube type bundle inserted into a shell, however, there is no tube side fluid present in the bundle. Instead, the bundle consists of electric heating elements arranged in a u-tube configuration attached to a flanged support plate which bolts to a heater shell. The removable bundle is electrically energized to create heat through electric resistance in the heating elements, and the process fluid flows through the shell side of the heater making direct contact with the immersed heating elements, causing the fluid to heat up.
Electric heating offers advantages in efficiency as high power factors convert nearly all electrical energy into heat, and precise heating via a uniform heat flux which is controlled to meet exact process needs. It aids decarbonization as electric heating does not produce emissions at point of use, thus reducing the environmental impact of heating equipment. Electric Heaters carry a low hazard risk due to the absence of combustion which significantly reduces hazards and, if properly certified, ensures a safe working environment. Low maintenance costs due to the lack of combustion ensuring less down time, and a smaller footprint requirement as electric heaters do not require fuel storage or complex piping, valves, pumps, monitoring or exhaust systems.
EHT’s are typically used in power duty ranges from 10 kW to 1 MW per bundle, with the option to include up to four bundles in a single heater shell, with supply voltages up to 600 VAC. They are well suited for single phase flow to heat a number of process fluids, and a non-exhaustive experience list of example applications is below. For higher power duties or two phase flow, an Electric Impedance Heater or a Radiant Furnace may prove to be better suited on a cost versus footprint basis.
Example Applications:
Air (Instrument or ambient)
Ammonia
Chlorination Gas
Fuel Gas
Hydrocarbons
Hydrogen
Natural Gas
Nitrogen
Oxygen
Reduction Gas
Catalyst Regeneration Gas
Steam
Surge Pot Gas
ACG fabricates EHT’s ranging in size from NPS 2.5 to NPS 42. Materials of construction vary according to process conditions. Heaters are generally designed for high operating temperatures to maximize heat duty per bundle, minimizing equipment footprint and the need for multiple parallel bundles. Very high design temperatures may limit which materials can be used.
Shell materials can be Carbon Steel, Low Alloy Steel Cr-Mo, Stainless Steel 304/316/321/347, Hastelloy C276, Monel 400, Inconel 600, or Incoloy 800/H/HT.
EHT bundles are typically Stainless Steel 321, Inconel 600, or Incoloy 800/H/HT.
ACG can accommodate Design Temperatures up to 1300 °F [700 °C] and Design Pressures up to 4,000 PSIG [275 Bar]. The heater shell and bundle are both pressure containing components that are governed by ASME Section VIII Division 1 in the United States, and relevant pressure vessel codes abroad. EHT’s are usually designed to ASME VIII Div 1 code and carry a U stamp.
While the heater bundle appears to have a tubesheet, it is designated as a Heater Support Plate and designed per ASME Section VIII Division 1 Mandatory Appendix 41, which was written specifically to address electric immersion heater design. ACG also follows UOP specifications for heater bundle design.
The heater bundle power junction box is NEMA/NEC rated for use in hazardous locations via CSA US certification in the United States and ATEX abroad. Power junction boxes are placed on the heater bundle with a standoff area between the heater support plate and the junction box to allow for ambient cooling and the use of low temperature wiring in the power junction box.
The the following parameters are considered for an electric immersion heater design:
Heating Element Sheath temperature limits
Maintaining turbulent flow
Maximum flow limits at the inlet/outlet nozzles and within the shell
Pressure drop limits across the heater
Spatial constraints at site
Flux limits and limits on the output of a single element
The proprietary programs that we use for design purposes account for all the above factors and additional considerations.
Once designs meeting the project requirements and our internal standards have been established, the alternatives are evaluated to achieve the optimum balance of reliability, operational performance, maintainability, and project economics, ensuring the selected solution is fit for purpose throughout its service life.
ACG’s EHT’s connect to customer supplied 3-Phase, low voltage supply power. ACG offers low voltage electric heaters (maximum 1,000 VAC supply power) as they provide a robust product that meets our commitment to equipment reliability.
The power output of an electric heater is defined as the Power = (Voltage^2)/Resistance. For a 4160 VAC medium voltage heater compared to a 480 VAC low voltage heater, the medium voltage heater would require a 75 times higher resistance than for the low voltage solution to generate the same power output, which can be achieved through either increasing the resistance of the individual heating elements or increasing the number of heating elements wired in series. A higher resistance heating element is made by decreasing the diameter of the resistance wire within the element, and a finer wire is more prone to failure at typical operating temperatures due to burnout. Alternatively, increasing the number of elements wired in series significantly decreases the fault tolerance of a heater as a series-connected configuration introduces a single-point failure mode, whereby failure of one element can render multiple heating circuits inoperative. In addition, a 4,160 VAC supply would require approximately seven heating elements to be connected in series to maintain element ratings and construction practices consistent with proven lower-voltage designs.
Medium voltage electric heaters offer benefits during the installation as they do not require a transformer from the operating site’s medium voltage supply to the heater’s low voltage, but the above tradeoffs introduce longevity issues that require more frequent bundle replacements resulting in increased downtime, reliability issues, and maintenance costs. The initial savings of avoiding a step-down transformer with medium voltage heaters are then likely offset by the more frequent replacement costs.
The element sheath to support plate welds are governed by ASME Sec. VIII Div 1 UW-20 and performed using an ASME Sec. IX qualified GTAW process in the same manner as a typical shell & tube exchanger weld. Welding the heating element sheaths to the support plate creates a robust leak free connection that can be validated through traditional non-destructive examination [NDE] methods such as dye-penetrant testing [PT] and hydrostatic testing. The welded connections contain the process fluid in the shell side where it belongs and results in a longer bundle life.
All ACG EHT heaters are 3-phase heaters. Our ability to meet certain kW ratings is limited based upon the resistance values of the Nichrome resistance wire in the heating elements. To achieve certain kW ratings the heater can either be wired as a Delta or as a Star in the terminal box. We typically wire the heater as a Delta but will sometimes wire as a Star to hit lower kW rating thresholds.
Our heater systems are preferentially configured in a delta arrangement due to its inherent reliability and fault tolerance characteristics. We design our heaters without the requirement of a system neutral. This is fine for Deltas because the risk of overvoltage is minimal in the case of a lost element (we still recommend rebalancing the heater if an element is lost in a Delta). In the case of a Star with no system neutral you will have a floating neutral. If you were to lose an element with a floating Star the risk of overvoltage to an element is greatly increased. Safety equipment can help mitigate this risk but a Delta in general is preferred
ACG also prefers delta wiring over a wye/star pattern as the delta configuration does not require a neutral point between supply power phases and thus requires less wiring, hardware, and a smaller footprint to install. It allows for a more compact and cost effective junction box.
Moisture ingress into the power junction box can lead to electrical shorts of the heating elements and loss in overall rated power duty to the heater or even lead to a scrapped bundle. This can be mitigated through the inclusion of an Anti-Condensation Heater located in the power junction box to prevent moisture buildup. The ACH is a low-voltage heater that can be set to energize at a predefined temperature above the expected dew point, thereby preventing condensation within the enclosure.
ACG also designs the heating elements themselves to resist moisture intrusion through two methods: 1) Each individual element end is dipped in a sealant and baked to create a hydrophobic seal between the electrical resistance element and the power connection, and 2) an epoxy sealant is applied on the end of the elements after the hydrophobic seal is established. The epoxy provides both electrical insulation and an extra layer of protection against moisture ingress.
The process fluid in EHT’s makes a single pass longitudinally along the length of the heater shell from the inlet nozzle to the outlet nozzle and directly contacts the immersed heating elements to transfer heat from the hotter elements to the cooler fluid. To achieve the maximum heat transfer for a given design, it is vital that the process fluid be in turbulent flow (mixing fluid) instead of laminar flow (smooth flow with no mixing), and the constant flux of the heating elements requires the elimination of stagnant fluid locations to avoid recirculation “dead zones” that would cause the heating elements to overheat and burnout. The heater is sized to ensure turbulent flow for a given set of process demands, and ACG also utilizes proprietary in-house designed grid style bundle supports that allow the fluid to flow through the full diameter of the shell. The grid style supports help maintain turbulent flow, eliminate recirculation zones, and reduce vibration concerns that otherwise would be present in a traditional segmented baffle style tube support. Our supports eliminate hot spots often found when segmented baffles are used.
Laminar flow is generally considered to be bad for electric heaters because the fluid movement is longitudinal (along the length of the pipe) only with no mixing. Essentially, the same layers of fluid around the elements are getting heated, while very little heat transfer is occurring between the different layers of fluid. Since electric heating is constant flux, this means that the fluid in contact with (or very close to) the elements will be heated to increasingly higher temperatures without any good avenue to transfer that excess heat to the bulk of the fluid. To achieve that constant flux, the heating elements will need to get much hotter than they would with turbulent flow and more normal heat transfer. This can cause the elements to burn out prematurely. It is important to note that the supports help to generate some turbulence but cannot be relied on to help enough to make laminar flow a viable option.
Thermocouples are included in all ACG EHT bundles to provide electric heater element temperature monitoring. The sensor ends of the thermocouples are welded or brazed to the heater element sheaths at the outlet end of the bundle near the highest expected temperature location, and the signal ends terminate in a thermocouple junction box attached to the power junction box for customer signal connections. Simplex (single sensor) and duplex (dual sensor – one extra sensor in the same thermocouple sheath that acts as a spare) thermocouples are available. Thermocouples can also be provided on the bundle support plate to monitor the temperature at the outside face of the support plate, or on the outside diameter of the heater shell to monitor shell skin temperatures. Typically a 4 – 20 ma signal is sent to a Junction Box and the signal is relayed to the Control Panel. Bundle thermocouples serve to indicate a high temperature event and the DCS can be set to trip the heater to avoid burnout at a preselected temperature if needed.
An electric radiant furnace provides indirect process heating to a pressure vessel, reactor, process piping, or coil to heat a process fluid by surrounding a pressure vessel and heating the vessel without penetrating the pressure boundary. A radiant furnace is typically made of three segments at 120 degrees which contain solid NiCr electric resistance heating elements which are attached by ceramic hangers to refractory insulation, usually composed of multiple fiber blocks. The segments are then assembled around the pressure vessel to be heated. When the furnace is energized, the elements generate heat through electric resistance which radiates onto the surrounded pressure vessel, heating the fluid inside. The annular design allows for high temperatures in the region between the furnace and the pressure vessel while the insulation keeps the outside surface of the furnace at temperatures safe for site personnel.
ACG can provide either a custom sized radiant furnace to assemble in the field around a vessel provided by others or a furnace pre-assembled with an internal pipe coil or ASME rated pressure vessel that the end user connects to their process piping in the field via flanged connections.
Radiant furnaces themselves are not ASME rated pressure vessels, but rather are enclosures supporting insulation and heating elements to heat an internal pressure vessel.
A radiant furnace has the advantage of indirectly heating a process fluid, which means that the electrical heating elements are contained within the furnace itself and not the pressure vessel which the furnace surrounds, so the elements never come into contact with the fluid. This makes the furnace an ideal choice for high temperature corrosive fluid services and two-phase fluid flow that could otherwise damage the heating elements in an immersion heater or exceed the temperature and duty requirements of an impedance heater.
ACG’s radiant furnaces are electrically energized compared with a traditional gas fired furnace, so they offer zero in plant emissions and reduced cost and footprint requirements compared with non-electric furnaces. The electrical heating elements offer precise temperature control with immediate temperature adjustments.
There are no moving parts to the furnace and the thick NiCr heating elements result in little maintenance downtime and a long service life.
A single heater can achieve temperatures up to 2192°F [1200°C] with power duties up to 16 MW at supply voltages up to 690 VAC. Multiple furnaces can be modularly added in series for greater duties. Such a furnace can achieve temperatures required for molten salt storage and pyrolysis applications and offers high heat capacities with a relatively small footprint.
The furnaces are energized by low voltage 3-phase supply power, with one leg of each phase connected to a resistance heating element circuit. The furnaces can be supplied in multiple segments with each segment containing a heating element circuit energized by one leg of the 3-phase power or with each segment containing a full 3-phase circuit depending on the required design. The furnace segments are assembled around a pressure vessel and bolted together to create 360 degrees of radiant heating evenly focused on the internal vessel.
A radiant furnace can accommodate vessels up to 13.5 ft [4.2 m] in diameter. The furnace enclosure is typically made of carbon steel with internally mounted mineral wool insulation supporting the NiCr heating elements.
Yes, ACG can design a radiant furnace to include a nitrogen purge on the power junction boxes and the heated internal furnace space surrounding the vessel. For furnaces with an integral process coil, a purge can be easily included without significant modification to the furnace geometry. However, for furnaces surrounding a reactor vessel, expansion joints must be included in the design, sized either by ACG or by the end user, to create a pressure seal between the furnace and the outside of the heated vessel. Significant differential thermal growth should be expected between the ambient temperature furnace enclosure and the heated pressure vessel located inside.
ACG can include in-house fabricated thermocouples mounted to the furnace enclosure which penetrate the internal insulation to monitor both the air temperature near the heating elements and the pressure vessel skin temperature. We can alternatively supply thermowells on the furnace casing for a customer to install their own thermocouples in the field.
Some pressure vessels have process or instrumentation connections located in the heated area that must protrude through the furnace casing. ACG can incorporate nozzle protrusions in the furnace design and provide expansion joints for field installation connecting the furnace enclosure to the pressure vessel nozzles to ensure a thermal break and weather resistant seal.
Cooling nozzle connections can also be supplied on the furnace enclosure to allow the end user to blow moving air through the heated space and reduce cool down times between furnace operation.
The furnaces typically fail by electrically shorting the resistance heating elements, usually through ambient water intrusion into the furnace’s insulation during installation or maintenance. This is not particularly common since ACG designs the furnaces to include a watertight seal on the segment seams and advises end users to ensure that the furnace and insulation is dry before energizing the heating elements. Shorted elements can be inspected or replaced.
Radiant furnaces are designed in multiple segments to be assembled around a pressure vessel and bolted together with a gasketed joint at each of the segment seams. Over-tightening the bolts along the segment seams can warp the segment flanges and open leak paths into the furnace for thermal heat to escape and for ambient moisture to intrude.
While we have encountered the above are failure modes, radiant furnaces typically have a 20 to 30 year service life given the robust heating element size and lack of moving parts.
An electric Impedance Heater is a unique type of process heater which provides direct heating of a pipe containing a process fluid without the use of immersed heating elements. A process fluid to be heated is contained within a small diameter pipe which acts as a pressure vessel. This may be of either serpentine or helical design, and an electrical supply is used to energize the pressure vessel itself. The electrical resistance of the pipe material causes the wall to heat up which, in turn, heats the process fluid as it flows through the vessel. Heat is provided directly from the vessel walls which allow significantly higher design temperatures and pressures than immersion heaters which utilize removable electric heater bundles. The coil pipe is contained within an insulated enclosure with all exposed surfaces grounded to ensure personnel protection.
These are specialized niche pieces of equipment for process demands such as supercritical fluids. We have also noted an increase in applications for high temperatures and pressures required while handling process fluids which are prone to fouling other types of heaters.
This equipment type has a relatively high initial cost but is very efficient with no moving parts or the need to replace bundles, thus offering low maintenance costs.
Low voltage customer supplied 3-Phase power (up to 690 VAC) is run through a step down transformer to create a lower voltage (120 VAC or less) / higher amperage load power that energizes the heater wall to achieve high design temperatures. Each transformer is custom designed for the heater duty and is included with the package, with each leg of the 3-Phase power used to energize sections of the heater wall.
As the electrical resistance of the heater wall material varies with temperature, ACG uses phase angle controlled 3-Leg SCRs to achieve precise temperature control ensuring the heater functions as the process requires. As the heater is electrically grounded inside an enclosure, there are no electrically energized exposed portions of the heater.
The heater contains no discrete heating elements that are susceptible to fouling, electrical failure, or burnout. Heat is generated directly within the pressure-retaining wall, eliminating a common source of maintenance and unplanned outages. The resulting design provides high operational reliability, low maintenance requirements, and simplified installation consisting primarily of electrical and process-fluid connections.
Individual Impedance Heaters are suitable for duties from 20 kW to 1.5 MW, and temperatures up to 1800°F [982°C], and design pressures up to 4700 PSIG [325 Bar]. The temperature and pressure combinations are quite high, which allow the heater to be used for supercritical fluid applications.
Typical process fluids include carbon dioxide, ammonia, water, hydrocarbons, and tar products. The heater is inherently well suited for two-phase and fouling services that can render conventional immersion heaters ineffective due to element fouling, overheating, or failure. This robust design delivers reliable performance in applications with severe operating conditions and challenging process requirements.
These can reach temperatures required for some molten salt applications and pyrolysis, which are growing applications within renewable energy storage and plastic recycling respectively.
Materials of construction are selected to satisfy both the process design conditions and the electrical resistance characteristics required for the heating duty. Heater shells are typically fabricated from 321 stainless steel, Hastelloy® C22 or C276, or Incoloy® 800H/800HT. The small-diameter coil construction accommodates high operating pressures while promoting uniform heat transfer to the process fluid. The coil assembly is housed within a custom enclosure up to 9.5 ft (3 m) in diameter and 12.5 ft (4 m) in overall height.
Impedance heaters provide efficient, reliable direct heating for demanding high-temperature and high-pressure process applications. Their design accommodates two-phase flow and fouling services that are often unsuitable for conventional electric immersion heaters. By eliminating discrete heating elements and directly energizing the process vessel wall, impedance heaters reduce maintenance requirements while delivering precise temperature control and uniform fluid heating for both established and emerging process technologies.
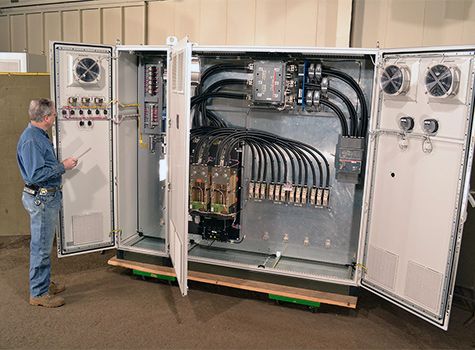
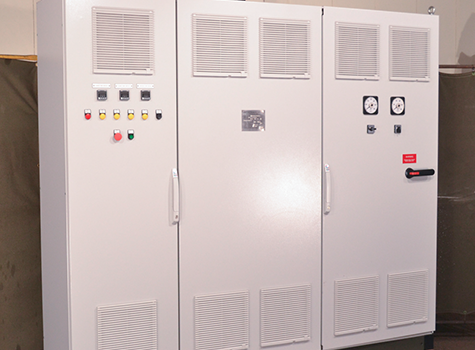
A control panel is used to provide electrical power, controls, and sensor connections to electrical equipment to allow the user precise monitoring and control of their electrical process heaters. ACG designs and fabricates customized control panels in house to accompany our electrical heating process equipment such as electric immersion heaters, impedance heaters, and radiant furnaces. We can supply them both as an accompanying piece of equipment to an electric heater or as a custom stand-alone item and can fabricate them to a customer’s requirements even if we have not fabricated the associated process equipment.
ACG can manufacture control panels in both the Coatesville USA and Beith UK locations with either CSA or ATEX certification as required by the end user’s local jurisdiction. Some components within the panels will differ based on the fabrication location and availability of subcomponents.
Panel Sizes: Depth is approximately to 24" and Height about 86". Width is technically unlimited with modular designs where multiple sections can be added side by side, but manufacturing and shipping become problematic for items wider than a 3 door design or about 117.5".
Material of Construction: The material of construction will depend on the required NEMA type enclosure rating. Type 12 is Carbon Steel with powder coating for use in an indoor non-corrosive environment. Type 4x is for outdoor use in a corrosive environment and is typically made of Stainless Steel 304 or occasionally Stainless Steel 316 when requested by a customer.
Area Rating: Armstong holds CSA and ATEX certification for non-hazardous areas and can self-certify for hazardous locations by including a nitrogen purge with 4X enclosure. CSA certification is used in the US & Canada, and ATEX is used in Europe and abroad. A non-hazardous location is one where explosive atmospheres (gases, vapors, or dust) are not expected to be present, while a hazardous location is one where explosive atmospheres are expected to be present, and the equipment must be designed to meet safety requirements for fire or explosion risk.
Indoor vs. Outdoor Installation: Indoor is non-hazardous typically designed to work in atmospheres up to 30 degrees C unless otherwise specified. Outdoor is designed for 40 degrees C unless otherwise specified. Area classification is determined by customer specification based on the local conditions and where the panel will be installed. Some customers locate the panels in a control room away from the process area where multiple pieces of equipment can be monitored simultaneously. Others locate the panel adjacent to the equipment in the process area allowing for direct hands-on monitoring and control. The different installation locations drive the requirements for the panel enclosure design and materials of construction.
UL Certification: ACG can certify to UL 508A under our CSA / CSA US Certificate for non-hazardous areas. We self-certify for hazardous areas, but those panels do not carry a UL certification.
Control: ACG can design a panel with Control Relays or a PLC. Both can be CSA certified. PLCs tend to be more expensive in components and design time.
Some Required Information would be: power duty requirement of the equipment to be controlled (heater kW rating), cable entry location (top or bottom of panel), area classification (if any), SCCR rating (typically can’t be higher than 100 kA and this also raises the cost of the main circuit breaker), customer required IO (especially in PLC applications). We can customize panels as required by customers.
While each control panel is designed for each specific piece of equipment, a standard Armstrong panel will typically include an SCR resistance heater control panel built for non-hazardous location in a control panel room with a type 12 enclosure. Included IO being a Digital ON/OFF signal and an Analog control signal to the SCR.
Type 4 and 4x enclosures, area classification rating, additional IOs, and PLC are available as upgraded designs.
ACG offers field service for equipment installation & troubleshooting the control panel as a part of sourcing an Armstrong panel.